

Product introduction
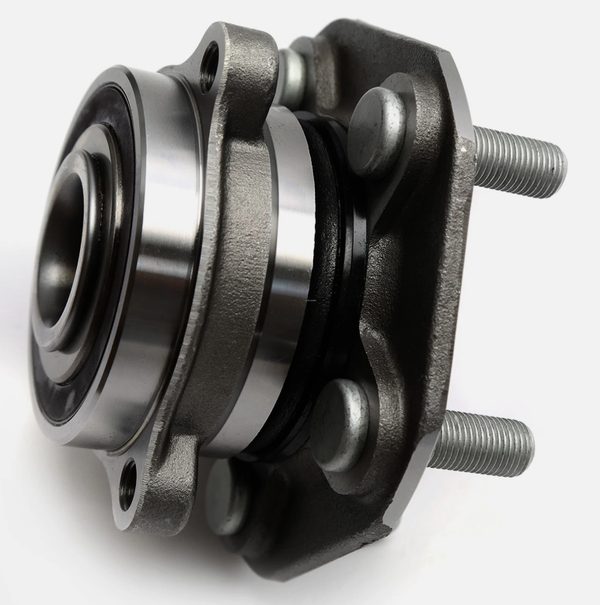
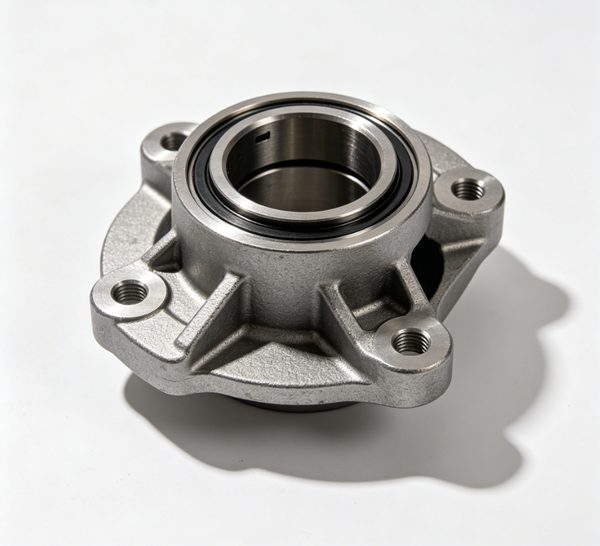
Ningbo Ruican manufactures air disc brake caliper brackets for commercial vehicles in ductile iron EN-GJS-500-7 (ASTM 65-45-12), with an optional 42CrMo4 alloy steel version for high-load axles. Casting is followed by CNC machining of slide-pin bores, caliper mounting faces and spring-loaded bushing seats so the bracket is delivered ready for assembly into the air disc brake system. Controlled microstructure, verified mechanical properties and machined datum control support the high fatigue strength required in truck, trailer and bus brake applications.
Specifications
| Parameter | Value |
|---|---|
| Casting process | Resin sand casting and silica sol investment casting; process selected by size, volume and tolerance |
| Casting weight range | 3.0 kg to 45.0 kg per piece |
| Dimensional tolerance | ISO 8062 CT4 to CT6 for silica sol; CT8 to CT10 for sand casting; machined features to drawing |
| Linear tolerance on machined features | +/- 0.02 mm to +/- 0.05 mm on bores and mounting faces, per drawing |
| Machining capability | 4-axis horizontal and 3-axis vertical CNC machining centers, CNC turning, boring, reaming, drilling, tapping, multi-face milling in one setup |
| Surface roughness | Ra 6.3 micrometers as cast; Ra 1.6 micrometers or better on machined sealing and bushing seats |
| Minimum wall thickness | 4.0 mm typical for ductile iron; 3.0 mm for investment cast sections subject to review |
| Key inspected characteristics | Slide-pin bore diameter, bore perpendicularity to mounting face, mounting face flatness, bushing seat depth |
| Heat treatment | Ferritizing anneal, normalizing or quench and temper, per material and drawing specification |
| Inspection | CMM, hardness tester, tensile and impact testing, ultrasonic testing, magnetic particle inspection as specified |
| Surface protection | Shot blasted, primer painted, e-coated or phosphated per customer specification |
| MOQ | 200 pieces for production orders; prototype and sample runs accepted from 20 pieces |
| Lead time | Tooling 25-35 days; samples 30-40 days; production 35-50 days after sample approval |
Key features
- Machined slide-pin bores with controlled diameter, roundness and surface finish, ensuring smooth caliper sliding and even pad wear over the service interval.
- Precision caliper mounting faces milled flat and square to the axle flange datum, holding brake torque reaction without fretting or bolt loosening.
- Spring-loaded bushing seats machined to controlled depth and concentricity, retaining the bushing under vibration and thermal cycling.
- High fatigue strength from a fully ferritic-pearlitic ductile iron matrix with verified nodularity, tested by tensile, hardness and impact testing per heat lot.
- Optional 42CrMo4 alloy steel version, quenched and tempered, for axle ratings where section size and load exceed ductile iron capability.
- Dimensional stability across production lots, supported by fixed tooling, defined machining datums and SPC on critical characteristics.
Applications
- Truck and tractor air disc brake systems on front and rear axles for long-haul and regional transport.
- Trailer and semi-trailer axle brake brackets supplied to axle and suspension assembly plants.
- Bus and coach air disc brakes, including low-floor city bus axles with compact bracket envelopes.
- Off-highway and construction vehicles where high brake torque and contaminant resistance are required.
- Aftermarket and remanufacturing programs requiring bracket interchangeability with original equipment dimensions.
Materials and heat treatment
| Material | Standard | Condition | Application note |
|---|---|---|---|
| Ductile iron EN-GJS-500-7 | EN 1563, ASTM A536 65-45-12 | As cast or ferritized annealed | Standard grade for air disc brake caliper brackets, balancing tensile strength, elongation and machinability |
| Ductile iron EN-GJS-600-3 | EN 1563, ASTM A536 80-55-06 | As cast, pearlitic matrix | Selected where higher strength and wear resistance are specified with reduced elongation |
| Ductile iron EN-GJS-400-18LT | EN 1563, ASTM A536 60-40-18 | Ferritic, low temperature impact tested | Chosen for cold-climate operation where low temperature impact toughness is required |
| Alloy steel 42CrMo4 | EN 10083-3, AISI 4140 | Quenched and tempered, typically 28-32 HRC | Optional high-load version for heavy axle ratings and severe duty cycles |
| Alloy steel 42CrMo4 | EN 10083-3, AISI 4140 | Quenched and tempered to 32-36 HRC | Used where bracket sections are reduced for weight saving and higher strength is needed |
Quality and compliance
Ningbo Ruican operates an IATF 16949 certified quality management system covering casting, heat treatment, machining and final inspection, with documented process control and full heat lot traceability from melt to shipment.
Process selection is driven by geometry, volume and tolerance: silica sol investment casting is used where tight tolerances to ISO 8062 CT4–CT6, fine surface finish and thin sections reduce machining allowance and overall cost, while resin sand casting is selected for larger brackets where section size and piece weight dominate. Ningbo Ruican confirms the route with you at quotation stage against your drawing and annual volume.
EN 10204 3.1 material certificates are issued for every shipment, covering chemical composition, tensile strength, elongation, hardness and impact values, together with the heat number and heat treatment batch. Mechanical test coupons are cast and tested alongside production parts.
First Article Inspection (FAI) reports provide full dimensional layout against ballooned drawings, with capability studies on critical characteristics such as slide-pin bore diameter and mounting face perpendicularity. PPAP-style documentation, including process flow diagrams, control plans, process FMEA, MSA results and run-at-rate evidence, is prepared under a customer Quality Agreement to support automotive and commercial vehicle programs.
Why Ningbo Ruican
- 17 years of casting experience in ductile iron, alloy steel and stainless steel, supported by in-house tooling, melting and heat treatment.
- One-stop production from casting through heat treatment, CNC machining, surface protection and inspection, reducing handoffs and lead time.
- OEM/ODM programs developed from drawings or physical samples, including DFM review, material selection and rapid prototyping in-house.
- IATF 16949 certified quality system with EN 10204 3.1 certification, PPAP-style documentation and controlled serial production.
FAQ
Which ductile iron grade suits an air disc brake caliper bracket?
EN-GJS-500-7 (ASTM A536 65-45-12) is the standard ferritic-pearlitic grade. EN-GJS-600-3 is used where higher strength and wear resistance are specified, and EN-GJS-400-18LT for cold-climate low-temperature impact duty. A 42CrMo4 quenched and tempered version covers heavy axle ratings.
How do you hold the slide-pin bore and mounting face geometry?
Slide-pin bores are machined to controlled diameter, roundness and surface finish, with mounting faces milled flat and square to the axle flange datum. Machined bores and faces hold +/-0.02 to +/-0.05 mm, with SPC on the key characteristics.
Can the bracket be supplied with surface protection?
Yes. Shot blasting, primer painting, e-coating and phosphating are all offered to customer specification, with coating thickness and appearance recorded on the inspection report.
What is the MOQ and lead time?
Prototype and sample runs are accepted from 20 pieces with a production MOQ of 200. Tooling 25-35 days, samples 30-40 days, production 35-50 days after sample approval. CMM, tensile and impact, ultrasonic and magnetic particle reports are available as specified.
CTA
Send your drawings to Wendy She at sales@cnsandcasting.com or WhatsApp +86 137 7712 4360 — include material grade, annual volume and target tolerance for a same-week quotation from Ningbo Ruican.
Website: http://www.cnsandcasting.com