


The clevis mount where the boom cylinder anchors to the backhoe loader’s main frame takes the full digging force of the machine on every cycle — often exceeding 40 tons of dynamic load. Welded clevis plates crack at the weld roots; the correct engineering answer is a single-piece ductile iron casting with continuous material through the load path and generous fillets at every section change.
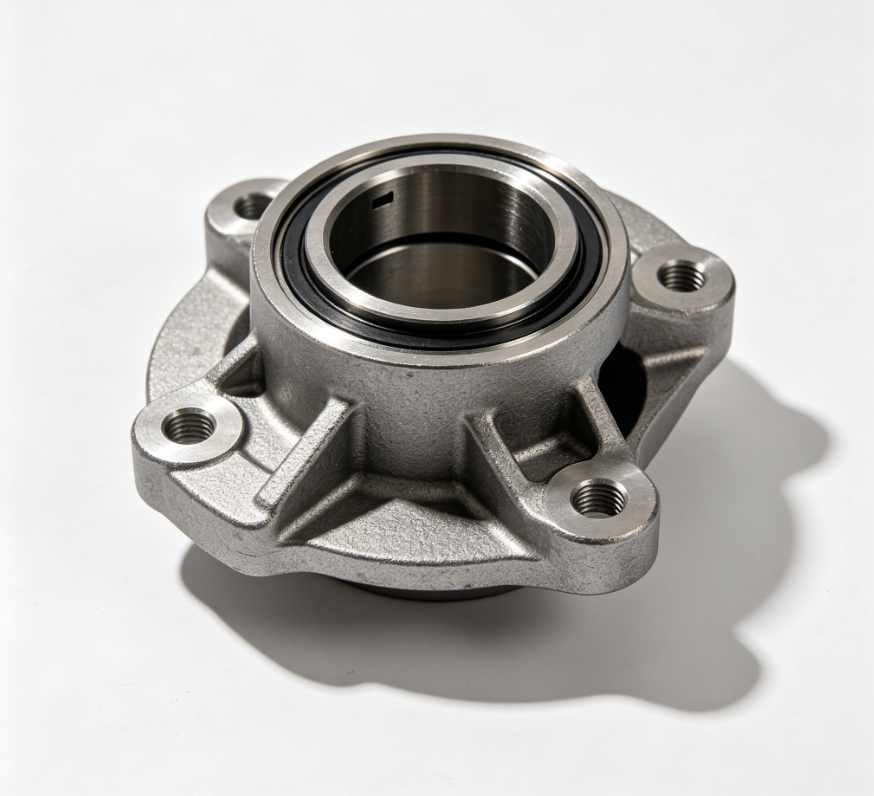
Ningbo Ruican casts backhoe boom cylinder clevis mounts in QT450-10 ductile iron (ISO 1083; equivalent to ASTM A536 65-45-12) by the investment casting process, delivering the compact clevis geometry — inner clevis ears, cross-pin bore, and gusseted base — near net shape. The fine-grain casting is then fully CNC machined at the cross-pin bore (typically H8 tolerance with surface finish Ra 1.6 µm) and mounting faces, ensuring correct cylinder alignment and pin fit.
For OEM machine builders and aftermarket parts distributors serving backhoe loaders in the 70–110 HP class, we produce clevis mounts to drawing with controlled microstructure verification (nodularity ≥ 80%, tensile and hardness tests per heat) and guaranteed dimensional repeatability across batches.
Key Specifications
| Parameter | Specification |
|---|---|
| Material | QT450-10 ductile iron (ISO 1083 / ASTM A536 65-45-12 equivalent) |
| Manufacturing Process | Investment casting + CNC machining |
| Heat Treatment | As-cast ferritic-pearlitic condition per QT450-10 |
| Mechanical Properties | Tensile ≥ 450 MPa, yield ≥ 310 MPa, elongation ≥ 10% |
| Pin Bore Tolerance | H8, Ra 1.6 µm (bushed or plain per drawing) |
| Weight Range | 3–25 kg depending on machine class |
| Inspection | Microstructure & nodularity check per heat, CMM dimensional, MT on request |
| Documentation | EN 10204 3.1 certificates with mechanical test results |
| Applications | Backhoe loaders 70–110 HP, mini-excavators, telehandler booms |
Ductile Iron + Investment Casting: The Right Combination for Clevis Parts
Sand casting ductile iron clevis mounts often needs 5+ mm of stock and still risks dross and shrinkage at the clevis ears — the thickest, most highly stressed section. Investment casting fills the ear geometry more uniformly, solidifies under controlled feeding, and delivers machined-ready bores with minimal stock. The result is a mount with consistent hardness, verified nodularity, and a pin bore that machines true on the first piece.
Why Choose Ningbo Ruican
- 17+ years casting cylinder mounts, clevises, and lug components for construction machinery
- Ductile iron grades from QT400-18 to QT700-2 plus cast steels for extreme-duty variants
- Integrated machining of pin bores, faces, and bushing seats to drawing tolerance
- Aftermarket kits: clevis mounts supplied with cross pins, shims, and bushings as matched sets
- IATF 16949 certified — process control culture proven in automotive-tier programs


Отзывы
Отзывов пока нет.