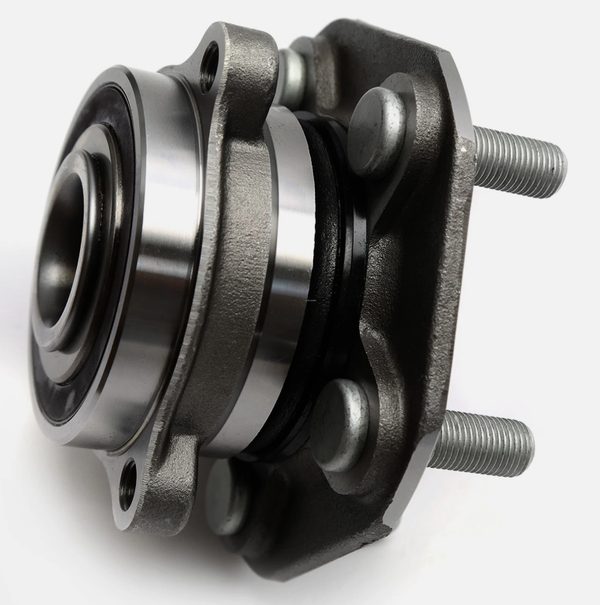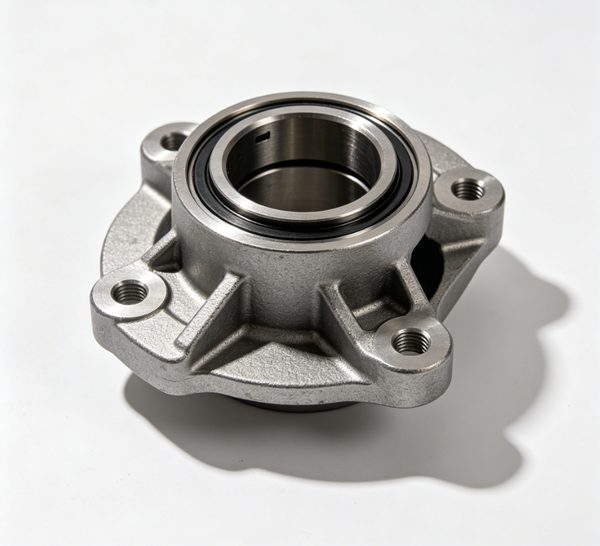


The bucket chain link body connects the buckets on the ladder of a bucket dredger, cutter suction dredger ladder chain or gravel recovery plant, and it runs through sand, gravel, clay and rock slurry for thousands of hours. It is a consumable wear part: the pin bores elongate, the link ears wear and the chain is replaced or re-linked during planned maintenance windows. Dredging contractors buy these links in sets, so repeatability between batches and short replacement lead time matter as much as wear life.
Specifications
| Parameter | Value |
|---|---|
| Material | ductile iron |
| Casting process | Investment casting |
| Surface treatment | Shot blast |
| Documentation | EN 10204 3.1 material certificate; PPAP / FAIR on request |
Material and Process
Moreover, this link body is a two-material design. Generally, the wear body is Mn13 Hadfield manganese steel, roughly 1.2 percent carbon and 13 percent manganese. This work hardens under impact and abrasion while staying tough in the core; it is water quenched from around 1,050 C to keep the carbon in solution. The mating carrier or pin boss part is EN-GJS-600-3 spheroidal graphite cast iron, which gives a strong, shock-damping seat for the pin and is easier to machine and replace. Both parts are produced by lost wax investment casting, water glass for the heavier manganese body and silica sol for the ductile iron carrier, then machined in-house.
Casting and CNC machining
- Tooling built to the approved model for each material.
- Wax injection and assembly, shell building in the selected system.
- Dewax, firing, melting and pouring with spectrometer control per heat.
- Shakeout, cut-off, riser removal, shot blast.
- Mn13 water quench from around 1,050 C; EN-GJS-600-3 heat treated to the specified matrix.
- CNC: mill the link ears and end faces, bore the pin bores, drill any grease or locking holes on 4-axis equipment.
- Deburr, hardness verification, layout inspection and pack.
Tolerances and Inspection
We hold casting dimensions to ISO 8062 DCTG 6 to 7 in the silica sol process and DCTG 8 to 9 in the water glass process, with machining allowance agreed at first article. We finish machined pin bores to drawing, commonly +/- 0.05 mm, with a parallelism callout across the two bores so the chain tracks true on the ladder. Inspection covers CMM or arm checks of bore spacing and ear thickness, Brinell hardness on the manganese body in the as-quenched condition, hardness on the ductile iron carrier, tensile results from heat coupons and OES chemistry per heat.
NDT and Documentation
Dye penetrant inspection on the manganese link body because fully austenitic manganese steel is not magnetic, and magnetic particle inspection on the EN-GJS-600-3 carrier body. We can quote ultrasonic testing on the heavy link sections and radiographic testing on the pin boss area where the buyer specifies them. Inspection and NDT are supplied to the buyer’s specified standard and acceptance level; Ningbo Ruican does not supply classification society approval. Documentation includes EN 10204 3.1 material certificate for both materials, water quench record for the manganese body, heat treatment chart for the ductile iron, dimensional report, NDT report and PPAP or FAIR on request.
Packaging and Logistics
Links are packed as matched sets so a contractor can re-link a length of chain without re-matching parts, protected with rust inhibitor, wrapped in VCI paper with desiccant and strapped into ISPM 15 heat-treated plywood crates marked with part number, heat numbers and drawing revision. Each set is labelled with its heat so wear life can be tracked by batch. Standard dispatch is FOB Ningbo, with air or express freight when a dredger is stopped waiting on chain parts.
RFQ Checklist
- Drawing or 3D model (STEP, IGES, DWG) with revision level
- Mn13 and EN-GJS-600-3 grades, hardness requirements
- Moreover, Dredged material type, chain pull and duty hours
- Number of links per chain and sets required
- Generally, Machining allowance and bore tolerance requirement
- NDT method and acceptance level as specified by the buyer
- Quantity, first article required and target delivery date
- Send drawings to Wendy She – sales@cnsandcasting.com – WhatsApp +86-13777124360
FAQ
Q1: Why combine Mn13 with EN-GJS-600-3 in one link assembly?
A1: Mn13 work hardens under the impact and abrasion of sand and gravel and stays tough in the core, while the EN-GJS-600-3 carrier gives a strong, shock-damping and easily machined seat for the pin.
Q2: Can you supply links as matched sets for one chain length?
A2: Yes. Additionally, links are packed and labelled as sets with their heat numbers. In general, a contractor can re-link a chain length without re-matching parts on site.
Q3: How is the manganese steel heat treatment controlled?
A3: The Mn13 body is water quenched from around 1,050 C to keep carbides in solution, then verified by hardness in the as-quenched condition, with the quench record issued against the heat.
Q4: Do you supply spare links for older dredger ladders without drawings?
A4: Yes. Send a worn link and we 3D scan it, rebuild the model with agreed machining allowance and datums, and produce a first article for fit and wear check before the batch.
CTA
Ningbo Ruican supplies OEM and ODM build-to-print castings and CNC machined parts from Ningbo, China, working to IATF 16949 and ISO 9001 with EN 10204 3.1 material certificates and PPAP or FAIR documentation. In general, typical part weight is 0.05 to 25 kg. Send drawings to Wendy She – sales@cnsandcasting.com – WhatsApp +86-13777124360, or visit https://cnsandcasting.com.