

We hold A watertight door closed by a row of dogs: each dog consists of a handle or lever, a shaft that passes through the door leaf. A wedge-shaped cleat that pulls the door against the knife-edge and the rubber gasket. The dog body described here is the cast and machined cleat and shaft boss that carries the actual clamping load. It sits immediately above or below the freeboard deck, in the splash zone, permanently wet with salt spray and periodically fully immersed. It is operated by hand after long intervals of standing still in a corrosive atmosphere.
That combination is why the part fails in two distinct ways rather than one. Corrosion seizes the dog, so it cannot be operated when it is needed. Wear of the wedge face means the door cannot be pulled onto the gasket hard enough to seal. These doors are inspected on a fixed cycle by whoever surveys or maintains the vessel. The operator’s practical requirement is simple. The dog must turn freely, pull the gasket to the specified compression, and be replaceable from stock without re-machining the door leaf.
Specifications
| Parameter | Value |
|---|---|
| Material | brass |
| Surface treatment | Passivation / Shot blasting |
| Documentation | EN 10204 3.1 material certificate; PPAP / FAIR on request |
Material and process
Standard grade is AISI 316L. For a casting the equivalent grades are CF3M per ASTM A351 or GX2CrNiMo19-11-2, supplied to the chemistry limits of the buyer’s drawing; the molybdenum-bearing austenitic structure is chosen for pitting and crevice corrosion resistance in chloride-containing water. The low carbon content keeps the alloy resistant to sensitisation if the part is welded to the door leaf or to a lever during installation.
316L is not itself subject to dezincification, and that is part of the reason it is specified here. On older vessels this component was made in brass or in a manganese bronze. Buyers now fit 316L or a dezincification-resistant alloy instead. Dezincification leaves a porous skeleton that looks intact but has no strength. Where the drawing still calls for a dezincification-resistant alloy rather than stainless, Ningbo Ruican quotes the bronze grade specified by the buyer and machines it to the same datum scheme.
Melting is by medium-frequency induction furnace with spectrographic control of each heat and records kept per heat number. We solution anneal the castings with the temperature, soak time and quench recorded, then descale, pickle and passivate them. That removes free iron from the surface and lets the passive chromium oxide film form evenly. Neglecting this step is the single most common reason stainless castings develop rust spots in the first weeks at sea. Where the drawing specifies it, a nitric or citric passivation route is used and the method is recorded. Note that austenitic stainless is non-magnetic, so magnetic particle testing cannot be used on this part and dye penetrant testing is used for surface inspection instead.
Casting and CNC machining
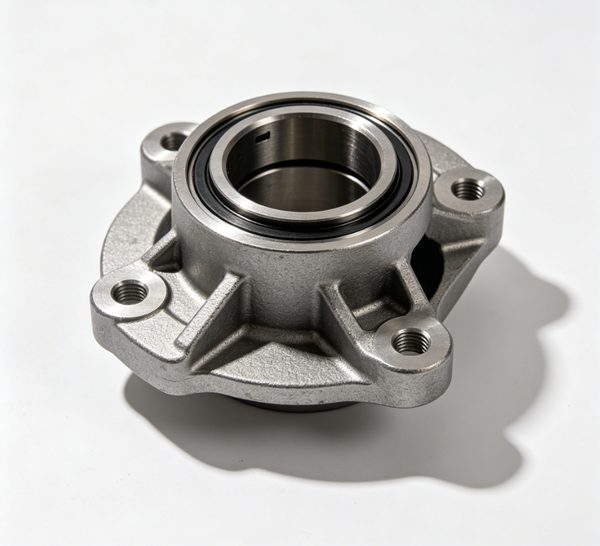
The dog body combines a shaft boss with an asymmetric wedge face. The wedge geometry is what makes it work. It also combines so the tooling is laid out with the feeder feeding into the boss and gentle choking so the metal does not erode the shell at the thin edge of the wedge. We normally use silica sol lost-wax: it gives the fine as-cast surface that reduces grinding on a part whose crevices would otherwise trap salt. It holds the thin wedge tip cleanly. Heavier bodies can run on the water-glass line when the drawing tolerance and surface requirement allow. After knock-out and shot blasting, risers are cut off, the parts are solution annealed, descaled, pickled and passivated, then passivated areas are protected before machining.
Typical route:
- OP10 – mill or turn the two locating faces that will register against the door leaf, establishing the datum for everything downstream.
- OP20 – machine the wedge or cam face to the specified profile and surface finish, holding the angle relative to the datum face.
- OP30 – bore or ream the shaft bore to the specified tolerance, and machine the keyway, flats or square drive that transmits the operating torque.
- OP40 – drill and tap any grease, locking or identification holes specified on the drawing.
- OP50 – deburr, break all edges to the drawing radius, remove any embedded iron contamination, wash with low-chloride water, dry, and passivate again if the drawing requires it after machining.
We build fixturing so all operations reference the door leaf contact faces, not the raw casting. This is what keeps replacement dogs interchangeable year after year.
Tolerances and inspection
We quote As-cast dimensional tolerance to ISO 8062-3, normally DCTG 6-7. After machining we hold the shaft bore to +/- 0.05 mm or to the specified fit grade. The wedge face angle stays at +/- 0.5 degrees or as stated. Datum face flatness stays within 0.1 mm, so the wedge loads the gasket evenly rather than on one corner. The relationship between the bore axis and the wedge face – which determines how far the door travels for a given movement of the handle – is held to +/- 0.1 mm and verified rather than assumed.
Machined surfaces are Ra 3.2 um with the wedge contact face Ra 1.6 um or better when specified, because a rough wedge face both abrades the receiving edge and needs more torque to operate. Verification is by CMM for angle and profile, by calibrated bore gauges and thread gauges, by a profilometer for roughness, and by hardness testing on the agreed scale and location. We perform positive material identification by portable spectrometer on finished parts when the drawing requires it, so mixed heats cannot reach the crate.
Quality & compliance
Surface inspection is by dye penetrant testing to ISO 3452-1. This is the applicable method for austenitic stainless steel, at the acceptance level and extent stated on the drawing; typical critical areas are the shaft-to-boss radii and the wedge root where the operating load concentrates. We offer radiographic testing or ultrasonic testing where the drawing calls for internal soundness evidence on the boss section. Ningbo Ruican does not hold or claim classification-society approval of this or any hardware item. We supply material chemistry and mechanical properties verified per heat. The pack adds dimensional inspection records and NDT reports against the buyer’s stated acceptance levels. A proof-load or operating test runs to the buyer’s procedure, with results recorded and witness attendance where required.
We deliver every shipment with EN 10204 3.1 material certificates tied to the heat number, plus the solution annealing chart. The pack adds the pickling and passivation record, the dimensional report and the NDT report. PMI records where specified and the packaging declaration close it out. First article inspection reports and PPAP submissions are available for serial programmes. Ningbo Ruican operates an IATF 16949 certified quality system with ISO 9001 aligned procedures.
Packaging and logistics
Stainless castings are easily contaminated by carbon steel handled with the same tools, which then rusts in service. We therefore segregate machined parts from carbon steel work. They are handled with non-ferrous or dedicated fixtures after the final pass, then wrapped individually in low-chloride VCI paper or polyethylene. Bores and threads are capped, wedge faces are protected with non-abrasive sleeves, and parts are boxed with dividers so nothing touches another surface in transit. We strap cartons onto ISPM 15 heat-treated plywood pallets with edge protection, and each carton carries part number, revision, heat number, quantity and the customer purchase order reference. A packing list with net and gross weights accompanies every shipment.
CTA
Send the following to get an accurate quotation and a realistic tooling lead time:
- 3D model (STEP or IGES) and 2D drawing (PDF or DWG) with revision level, datum scheme and wedge angle call-out.
- Door type, door leaf thickness and whether this is a new build, a replacement or a stocked spare.
- Material grade and cast equivalent agreed by the buyer: CF3M, GX2CrNiMo19-11-2, or an agreed dezincification-resistant bronze alternative.
- Surface finish requirement on the wedge face and shaft bore, and whether a finer finish is specified for reduced operating torque.
- Post-machining treatment requirement: pickling, passivation method, pickling paste restrictions, or iron contamination controls.
- NDT extent, method and acceptance level as stated on the drawing.
- Any operating torque, proof-load or cycle-test requirement, and whether the buyer requires witnessed testing.
- Documentation set: EN 10204 3.1, PMI records, FAIR or PPAP level.
- Mating edge or frame material, if the buyer wants Ningbo Ruican to comment on wear and galvanic behaviour rather than simply machine to print.
- Annual volume, batch size, call-off pattern, first-piece date, packaging marking and Incoterm.
FAQ
Why not machine this component from bar rather than cast it?
Because the wedge and boss can be cast near net shape, the machining is confined to the faces that matter. This keeps unit cost down at volume and keeps grain flow continuous around the loaded corner rather than cutting across it. For one-off prototypes Ningbo Ruican will quote machining from bar or plate if that suits the quantity.
Can you supply a dezincification-resistant bronze instead of stainless?
Yes, if the drawing specifies it. Ningbo Ruican works to the buyer’s stated grade and datum scheme, so a bronze alternative to an older brass or manganese bronze design can be produced as a drop-in replacement on the same fixture.
How is stainless handled so it does not rust in service?
Segregation after the final pass, dedicated fixtures, low-chloride wash water and documented pickling and passivation with the records included in the shipment set. Embedded iron from shared tooling is the usual cause of early rust spotting on stainless castings.
What comes with each shipment?
EN 10204 3.1 certificates tied to heat numbers, the solution annealing chart, pickling and passivation records, dimensional report, PT report per ISO 3452-1 to the buyer’s acceptance level, PMI records where specified. The test report for any proof-load or operating cycle test specified by the buyer.